How to Reduce Bone Dust When Using a Meat Band Saw

Table of Contents

Bone dust cannot always be eliminated when cutting bone, but it can usually be reduced through correct blade selection and condition, stable product preparation, controlled feeding, proper guide and tension settings, and a disciplined cleaning routine.

The short answer: control the cutting source
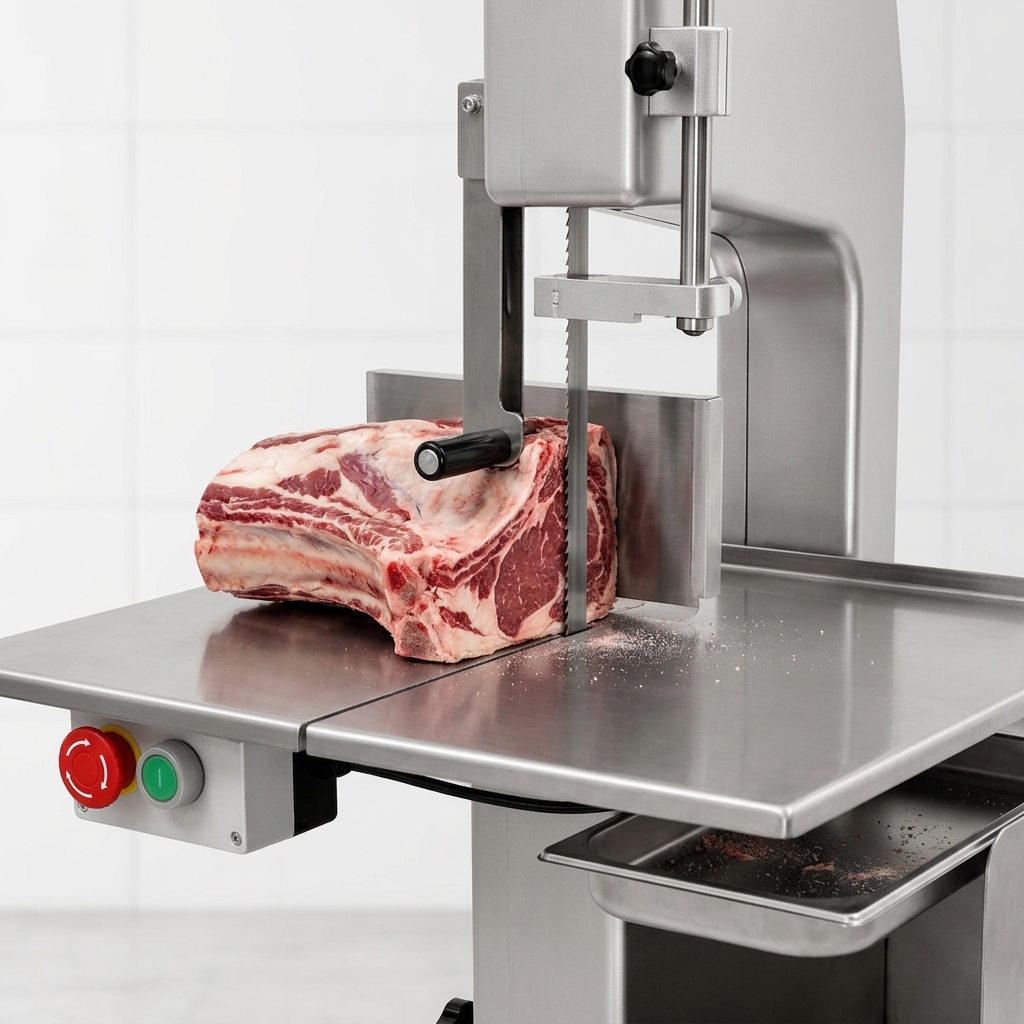
Controlled setup for cutting bone-in meat on a commercial band saw

To reduce bone dust when using a meat band saw, use a sharp and suitable blade, keep the product stable and properly chilled, feed it through the blade at a steady rate, and keep the saw correctly adjusted and clean. Bone dust is usually created when the blade crushes, rubs, wanders, or tears through bone instead of making a controlled cut.

Some fine bone particles are a normal result of cutting bone-in meat, especially on dense or irregular bones. The practical objective is not to promise a completely dust-free cut. It is to minimise visible residue, prevent it from spreading around the cutting area, and remove it safely before the product moves to the next process.

For commercial operators, this starts with a documented routine. Inspect the blade and guides before production, prepare product consistently, train staff to avoid forceful feeding, and clean the machine at the right intervals. These basic controls also support safer operation. Review the commercial bone saw safety and maintenance protocols alongside your machine manual and site procedures.

What causes bone dust on a meat band saw?

Bone dust is the fine residue and small fragments released at the cut line. It can remain on the meat surface, collect on the table, or enter seams and hard-to-clean areas of the saw. Larger chips and splinters are related concerns, but they are not exactly the same as fine dust.

The most common causes are mechanical and operational:

  • A dull or damaged blade: A worn cutting edge rubs and crushes material, increasing friction and fragmented residue.
  • An unsuitable blade pattern: Blade tooth form and spacing should suit the product, including its bone density, cut size, and whether it is fresh or tempered. A one-size approach may not produce the cleanest result on every item.
  • Incorrect tension or guide alignment: A blade that is not set according to the machine manufacturer’s instructions can deflect or vibrate during the cut.
  • Forced or uneven feeding: Pushing too hard can cause the blade to bind, while twisting the product can pull the cut line away from the intended path.
  • Unstable product: Loose pieces, uneven surfaces, and thawed or soft product are harder to control and can lead to chattering at the bone.
  • Poor housekeeping: Dust from an earlier cut can be transferred to subsequent portions if the table, guides, pusher, and surrounding area are not cleaned promptly.

Look at the pattern, not just the amount. Residue concentrated on one side may point to drift, guide wear, or uneven feeding. A sudden rise after a consistent production period may indicate a blade that needs inspection or replacement.

Start with the right blade condition and specification
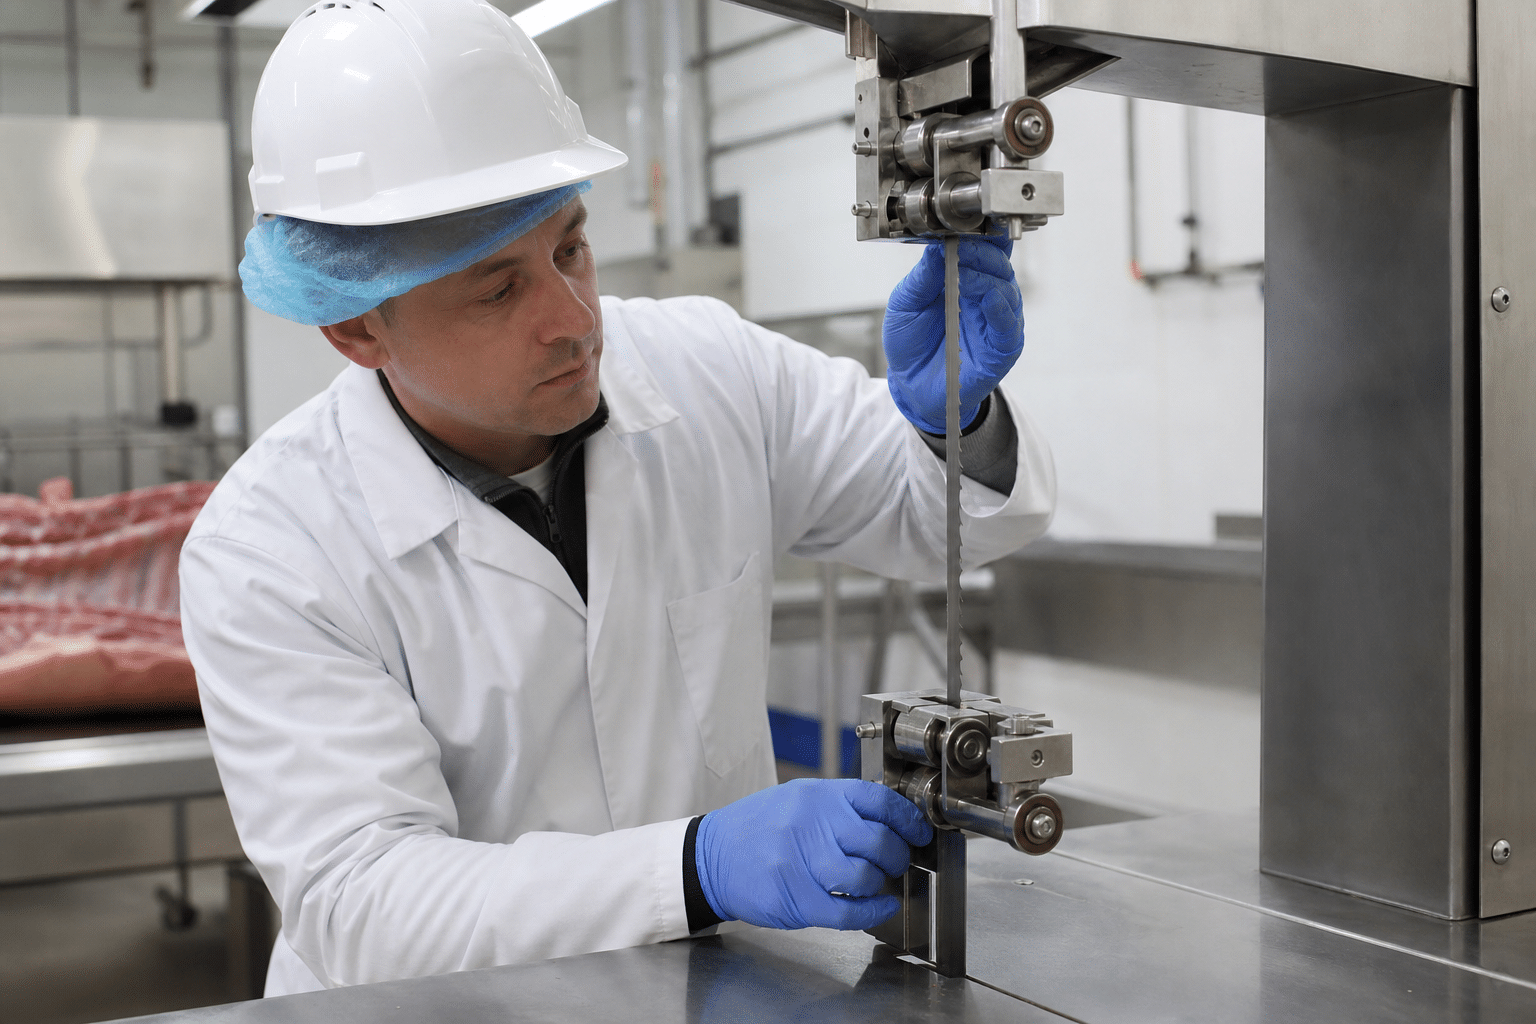
Inspection of a meat band saw blade and guide assembly

Blade condition is one of the strongest controllable factors in bone-dust reduction. Inspect a blade before use and whenever the cut quality changes. Replace a blade that is visibly damaged, has missing or bent teeth, shows corrosion, tracks poorly, or requires extra force to cut. Continuing to use a poor blade can increase residue and make the operation less predictable.

Select the blade specification using the saw manufacturer’s approved range and the actual products being cut. Discuss tooth configuration, blade width, and material with the blade supplier or equipment provider. The correct choice depends on factors such as whether you cut poultry, ribs, joints, frozen blocks, or other bone-in portions. Do not assume that a blade that performs well on one product will be ideal for all products.

Install and tension the blade only as stated in the equipment manual. Over-tensioning can place unnecessary stress on the blade and machine components. Under-tensioning can contribute to blade wander and vibration. After fitting a blade, confirm that it tracks correctly and that the guards are in place before production begins.

If repeated dust problems coincide with frequent blade changes, tracking difficulty, or inconsistent cuts, inspect the full system rather than blaming the blade alone. The commercial bone saw buying checklist for butchers is also useful for reviewing blade compatibility, cleaning access, service requirements, and the overall fit of a saw for your workload.

Prepare meat and bone for a cleaner cut
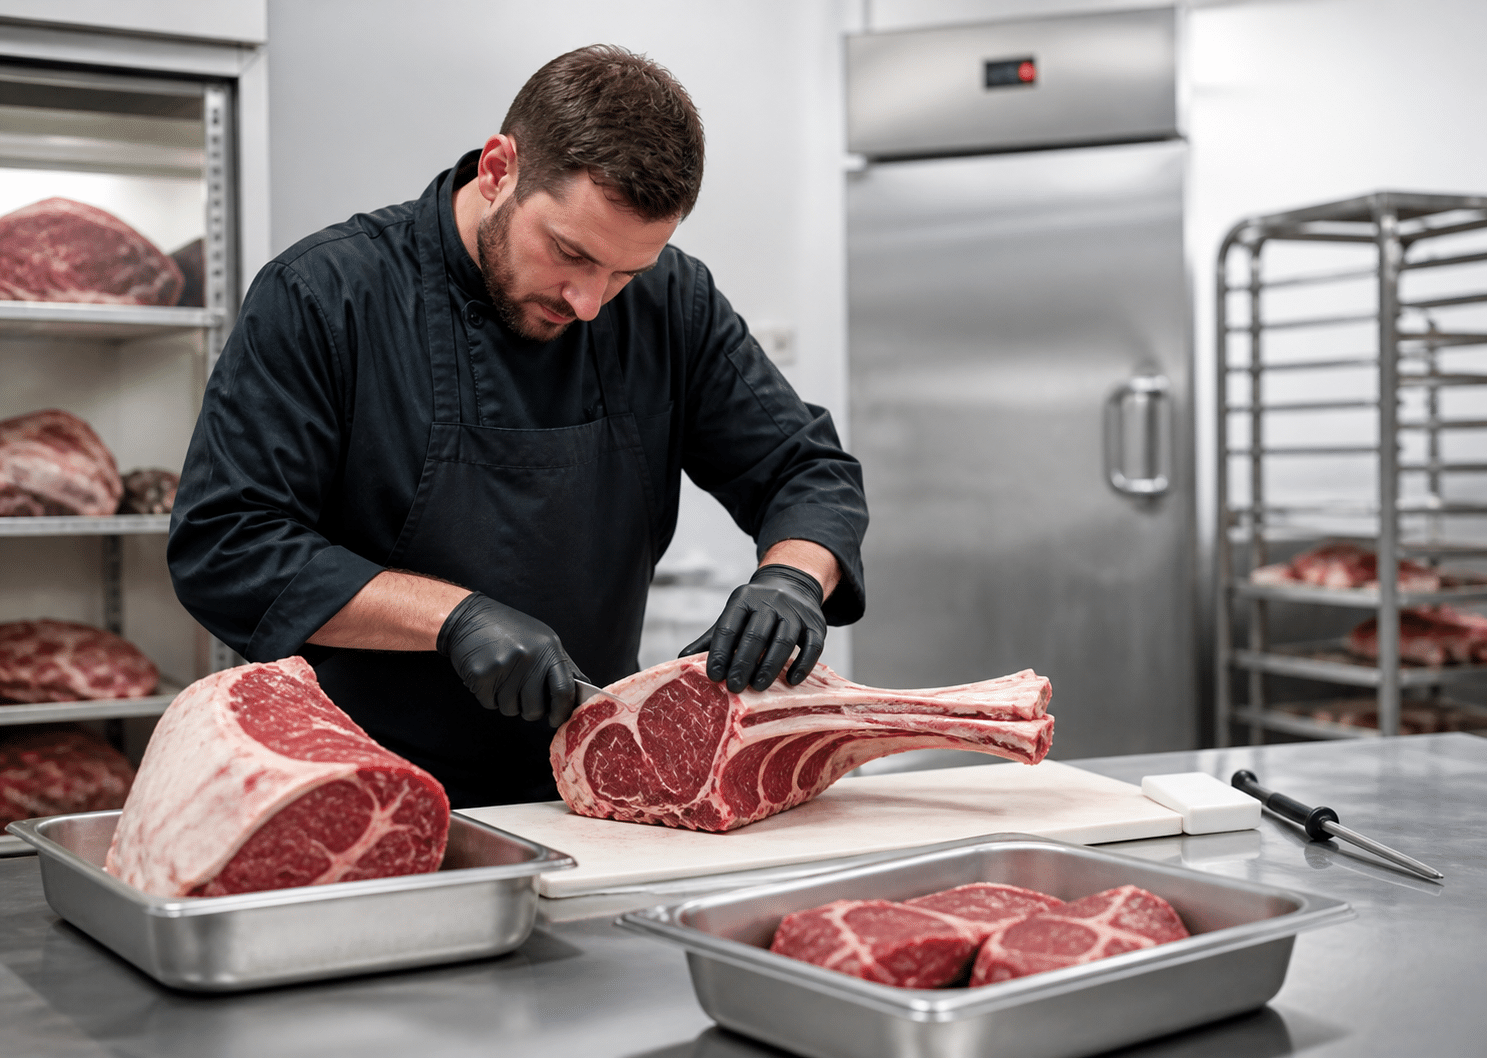
Chilled bone-in meat prepared for stable band saw cutting

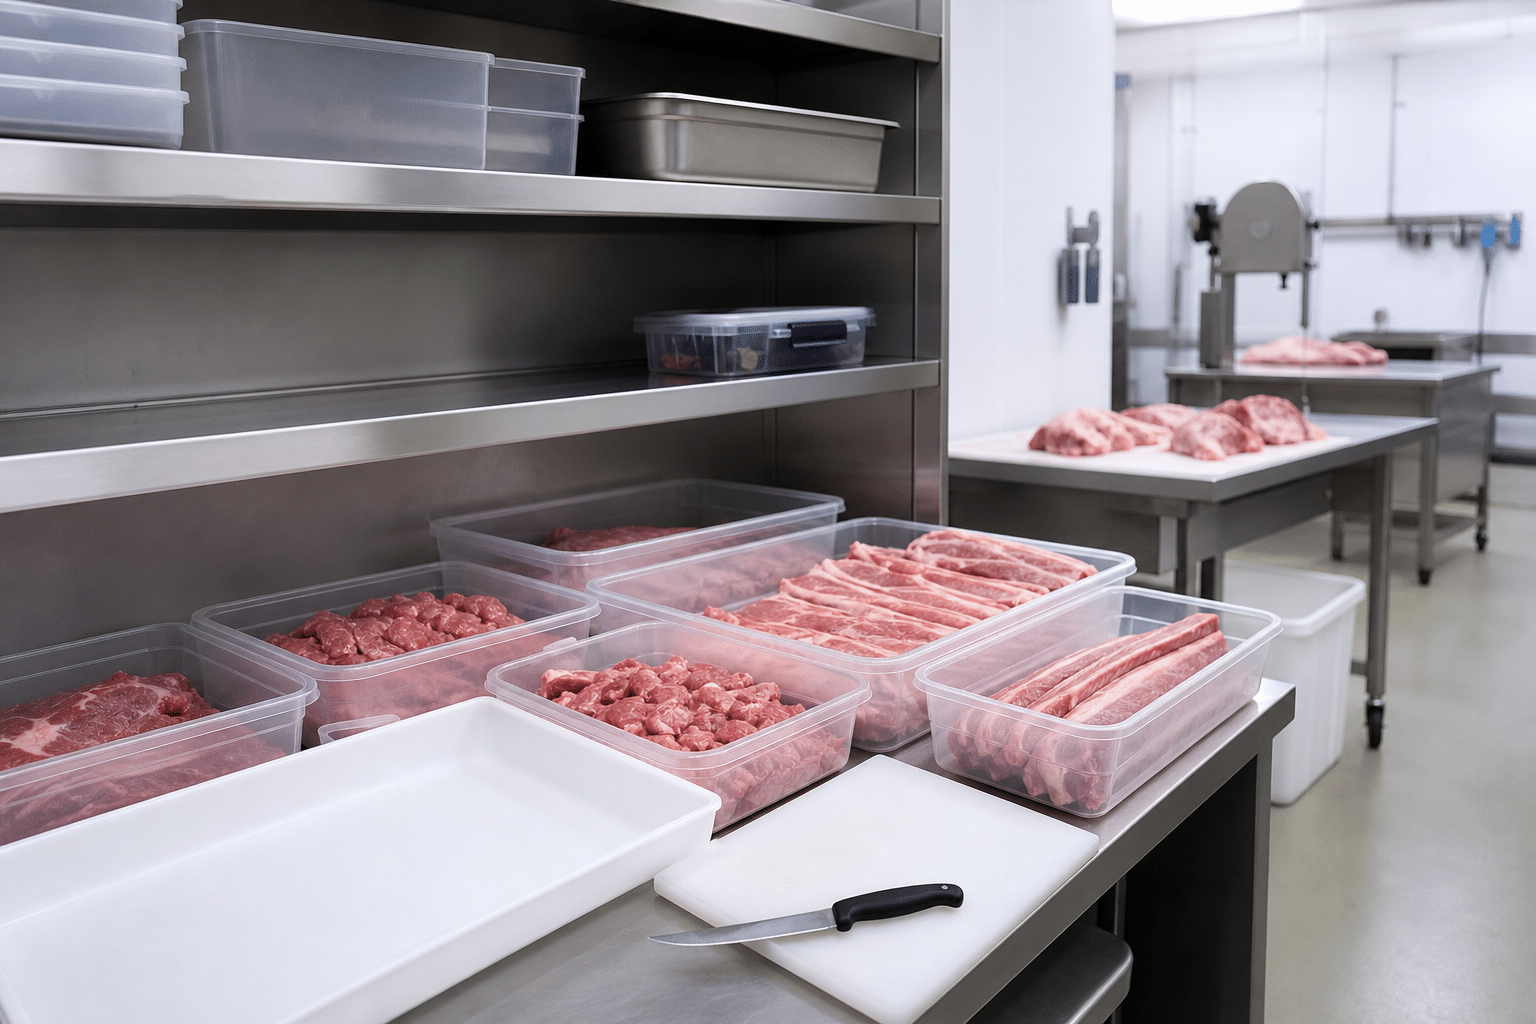
Product condition affects how smoothly the blade enters and exits bone. Prepare items to create a stable, repeatable presentation on the saw table. Remove loose packaging, ties, labels, and any non-product material before cutting. Check for foreign objects and separate product that is outside your planned cutting condition.

Keep product within the temperature range required by your food-safety plan and local rules. In many operations, firmer, well-chilled product is easier to hold and cut consistently than product that is soft or partially thawed. However, the right condition depends on the specific protein, cut, and process. Avoid using temperature changes solely to solve a cutting problem without checking product-quality and food-safety requirements.

Trim loose flaps where appropriate, and place the broadest stable surface on the table. For irregular joints or small pieces, use an approved pusher or holding device rather than trying to hold the product close to the blade. Never use hands or improvised tools to force the item through the cut.

Plan the cut line before starting. A deliberate route through the bone reduces mid-cut stopping, twisting, and re-cutting. Where an item must be divided into multiple portions, decide the order that maintains the best support for the remaining piece.

Use controlled feed technique

A well-maintained saw can still create excess bone dust if the product is fed poorly. The operator should guide the product smoothly into the blade with consistent, moderate pressure. Let the blade cut; do not use sudden force to overcome resistance.

Keep the product flat and supported on the table. Feed it in a straight line, without rocking or twisting. Turning a joint while it is already engaged with the blade can widen the kerf, create friction, and leave a rougher surface. If the piece moves unexpectedly, stop feeding, move it safely clear as allowed by the procedure, and reposition it before continuing.

Use the fence, gauge, pusher, or other approved accessory when it helps maintain a repeatable position. This is particularly important for portion cutting, where a consistent setup can reduce both operator variation and unnecessary rework. Set the upper blade guide as close as practical to the product while retaining safe clearance, following the machine instructions.

Operators should treat an unusual cutting sound, vibration, increased resistance, or a change in cut appearance as a reason to pause and inspect. These signs may indicate blade wear, guide adjustment issues, product movement, or a developing mechanical fault. Continuing through the problem usually creates more waste and more cleaning work.

Check machine setup, guides, and work area

Before the shift, check that the saw is stable, the table is clean, and the work area provides enough room to load, cut, and remove product without crowding. Poor workspace flow can encourage rushed handling and awkward product angles.

Inspect the blade guides, guide adjustment mechanism, blade scrapers where fitted, wheels, door closures, and guards according to the manufacturer’s maintenance instructions. These parts help control blade travel and contain residue within the intended cutting area. Do not remove guards, bypass interlocks, or modify the machine to gain access or speed up cleaning.

Confirm that the fence or gauge is secure if it is being used. A loose or poorly positioned guide can cause inconsistent portions and repeat cuts. Check that product trays and collection containers are placed so that cut pieces can be moved without passing over unclean areas.

Only use an extraction or collection method if it is designed for the equipment and accepted by your food-safety and workplace-safety procedures. An improvised vacuum attachment may obstruct the work area, create a cleaning issue, or interfere with the machine. Never use compressed air to blow bone dust from a food-processing saw; it can spread residue into the air, onto nearby surfaces, and into areas that are difficult to clean.

Remove dust safely and clean between tasks
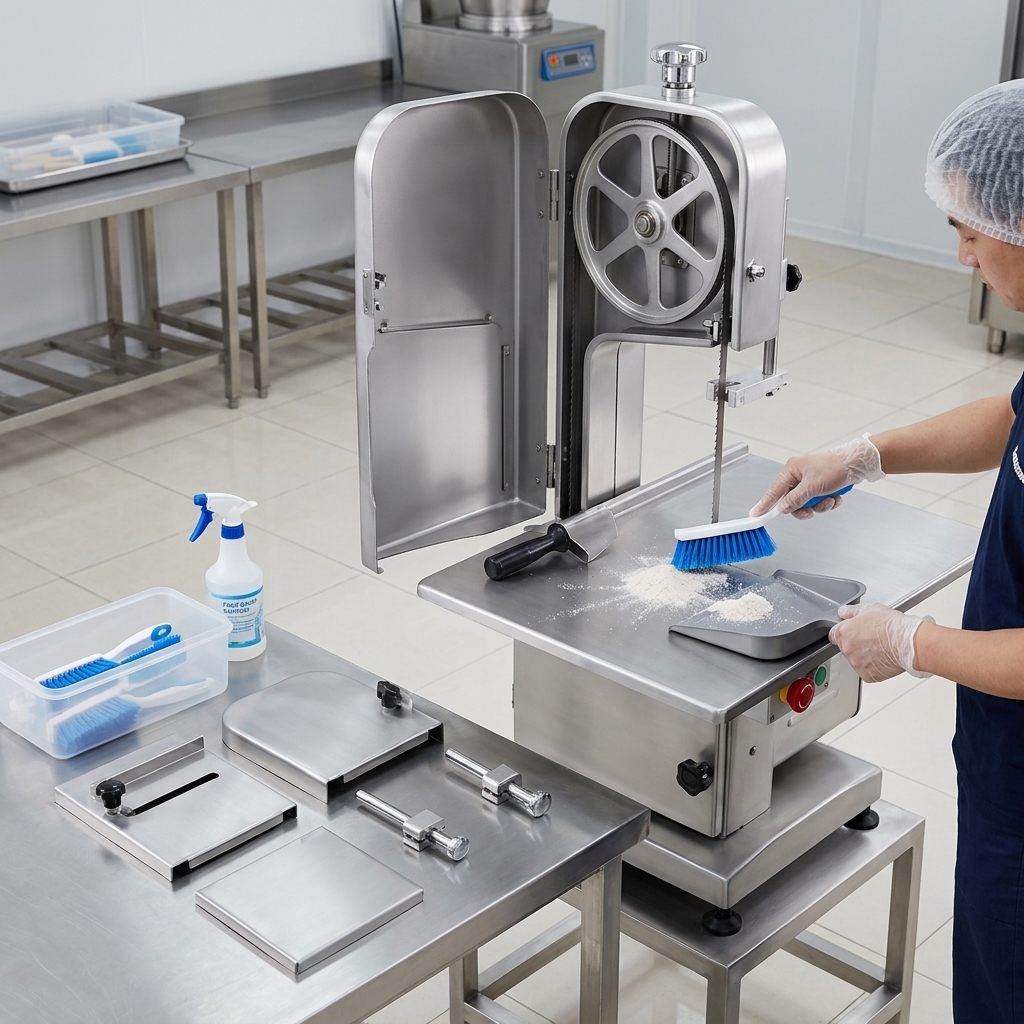
Safe cleaning of a commercial meat band saw after bone cutting

Dust control is incomplete if residue remains on the machine or is carried onto finished portions. Build cleaning into the production routine rather than waiting until visible buildup is heavy. The frequency should reflect the products handled, production schedule, local requirements, and your site sanitation plan.

Before cleaning, stop the machine, isolate it from its power source, and follow the lockout or isolation procedure required at your site. Wear suitable protective equipment. Use tools that are approved for the task to remove visible debris from the table, fence, pusher, blade area, collection points, and accessible guards. Treat the blade as sharp even when it is stationary.

Then clean and sanitise the machine according to its manual and your validated sanitation procedure. Food-contact surfaces, splash zones, and residue collection areas all need attention. Avoid directing high-pressure water at bearings, electrical parts, or areas that the manufacturer identifies as unsuitable for washdown. Reassemble the machine correctly, check that all guards are secure, and allow required surfaces to dry or drain before restarting.

The cleaning sequence of remove residue, wash, rinse, sanitise, and inspect is a useful operating principle across food equipment. For a broader example of structured sanitation controls, see this guide on cleaning and sanitising commercial food-processing equipment. Always adapt the procedure to the bone saw manual, chemicals in use, and your own food-safety plan.

Common mistakes that increase bone dust

The following practices often make a bone-dust problem worse:

  • Waiting too long to replace a poor blade. Extra feed pressure is not a substitute for a sharp, properly selected blade.
  • Using the same settings for every product. Different bone-in products may need different blade choices, guide positions, or handling methods.
  • Cutting unstable pieces without a pusher or support. Product movement causes inconsistent cuts and raises safety risks.
  • Twisting the product during the cut. This increases blade side loading and can create rough edges and residue.
  • Allowing residue to accumulate. Existing dust can spread to later cuts and conceal areas that need cleaning.
  • Blowing debris away with air. This spreads contaminants instead of removing them under control.
  • Ignoring recurring machine symptoms. Blade drift, vibration, rubbing noise, or poor tracking need investigation before they become a larger maintenance issue.

Record recurring issues by product type, operator, blade batch, and shift where practical. This makes it easier to distinguish a training issue from a blade-selection or machine-condition issue. A short log can be more useful than relying on memory when deciding what to change.

Daily checklist for lower bone dust

Use this practical checklist at the start of production and whenever cut quality changes:

  1. Confirm the blade is clean, undamaged, sharp enough for the job, and correctly installed.
  2. Check blade tracking, tension, guides, guards, table condition, and cutting accessories according to the machine manual.
  3. Prepare product at the required handling condition and remove packaging or foreign material.
  4. Set up the fence, gauge, pusher, and product collection area for a stable, direct workflow.
  5. Make the first cuts with controlled feed pressure and inspect the cut surface and residue pattern.
  6. Pause if the saw vibrates, pulls to one side, requires unusual force, or leaves a noticeably rough cut.
  7. Remove residue using the approved isolation and cleaning procedure at planned intervals and between incompatible tasks.
  8. Record blade replacement, adjustments, cleaning, and unresolved defects for the next shift or maintenance team.

A consistent routine helps operators reduce avoidable bone dust without compromising safe handling or sanitation. The correct final settings will always depend on the individual saw, blade specification, product type, and operating procedures supplied by the manufacturer and your site.
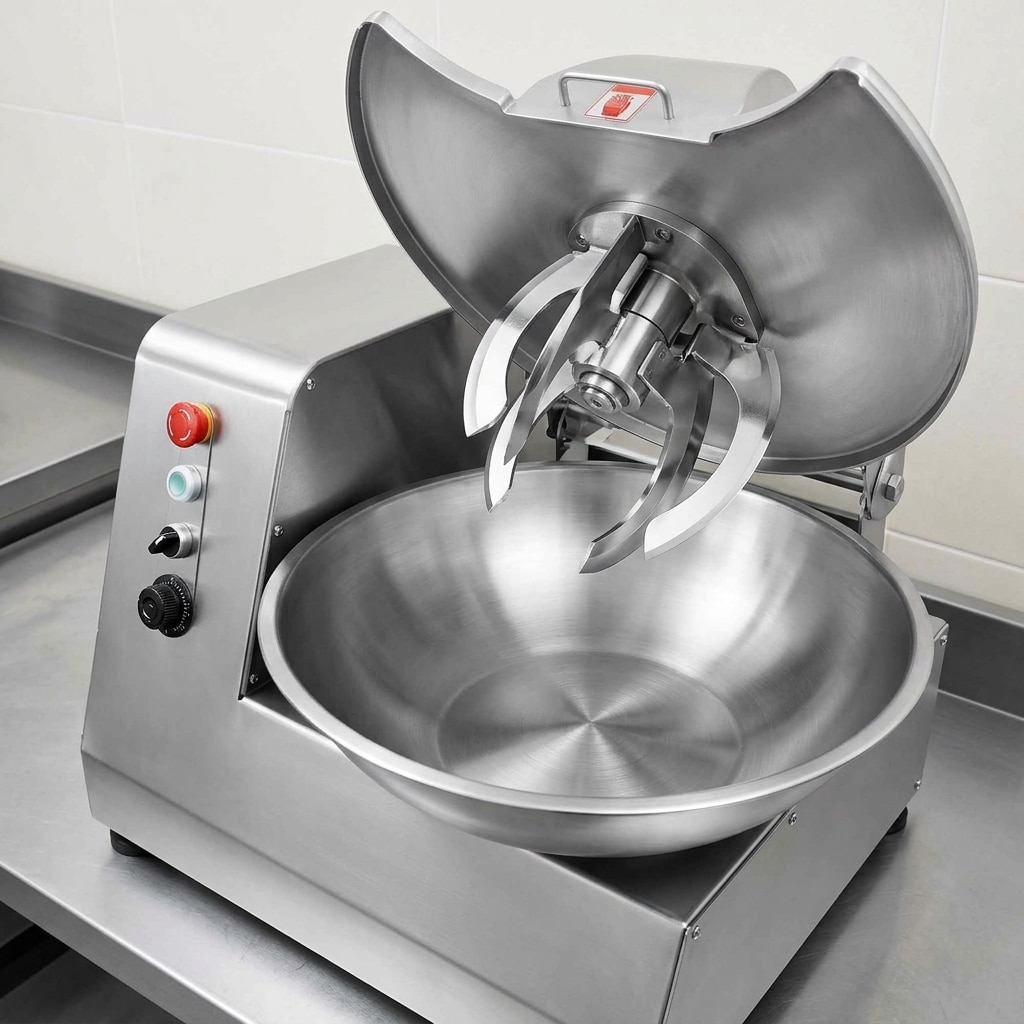
How to Prevent Bowl Cutter Blades From Dulling Early

Table of Contents

Bowl cutter blades dull early most often because of abrasive ingredients, hard foreign material, incorrect cutting technique, poor cleaning, or delayed sharpening. A controlled daily routine helps protect edge life and maintain a consistent cut.

The Short Answer

Clean bowl cutter blades ready for inspection

The best way to prevent bowl cutter blades from dulling early is to control what enters the bowl, use a cutting process that matches the product, clean blades with non-abrasive methods, and inspect the edge before it becomes noticeably worn. Blades should not routinely contact bone, metal, packaging clips, hard frozen blocks, or other foreign material unless the machine and blade specification expressly allow it.

For daily operation, keep ingredients within the machine’s intended preparation range, avoid forcing overloaded batches, use the correct blade speed and process sequence for the recipe, and remove residue soon after production. When an edge no longer produces a clean, even cut, arrange professional sharpening or replace the blade rather than continuing to run it.

Blade condition affects more than appearance. A sharp, intact edge supports predictable chopping, mixing, emulsifying, and batch handling. It can also help operators avoid extending cycles simply to compensate for a dull blade.

What Causes Bowl Cutter Blades to Dull Early?

Operator checking ingredients before bowl cutter processing

Early dulling is usually an operating or handling issue rather than a single equipment fault. Understanding the cause makes bowl cutter blade maintenance more effective.

  • Hard contamination: Bone fragments, metal clips, staples, wire, stones, broken packaging, and other hard debris can chip or roll an edge immediately.
  • Unsuitable product condition: Product that is excessively frozen, poorly trimmed, or presented in pieces beyond the cutter’s intended preparation method places high shock loads on the blades.
  • Abrasive ingredients: Certain spices, mineral-containing ingredients, coarse salt, and dry particulate ingredients can increase wear. This does not mean these materials cannot be processed; it means the recipe, sequence, and cleaning plan need attention.
  • Contact with the bowl or accessories: Incorrect blade clearance, a damaged bowl, loose hardware, or an incorrectly fitted assembly can allow unwanted contact. Stop the machine and investigate rather than continuing to operate.
  • Overprocessing: Repeatedly extending a cycle after the desired texture has been achieved creates unnecessary edge exposure, heat, and friction.
  • Incorrect cleaning tools: Abrasive pads, harsh scraping, careless stacking, and contact with other metal parts can damage a sharpened edge outside production.

Commercial bowl cutters are used for high-volume preparation because they combine chopping and mixing in one workflow. For a broader overview of where this equipment fits, see how commercial bowl cutters support high-volume food preparation. The exact blade, batch size, and process settings should always follow the machine supplier’s instructions and the approved recipe.

Prepare Products Before They Reach the Bowl

Prepared ingredients for a commercial bowl cutter

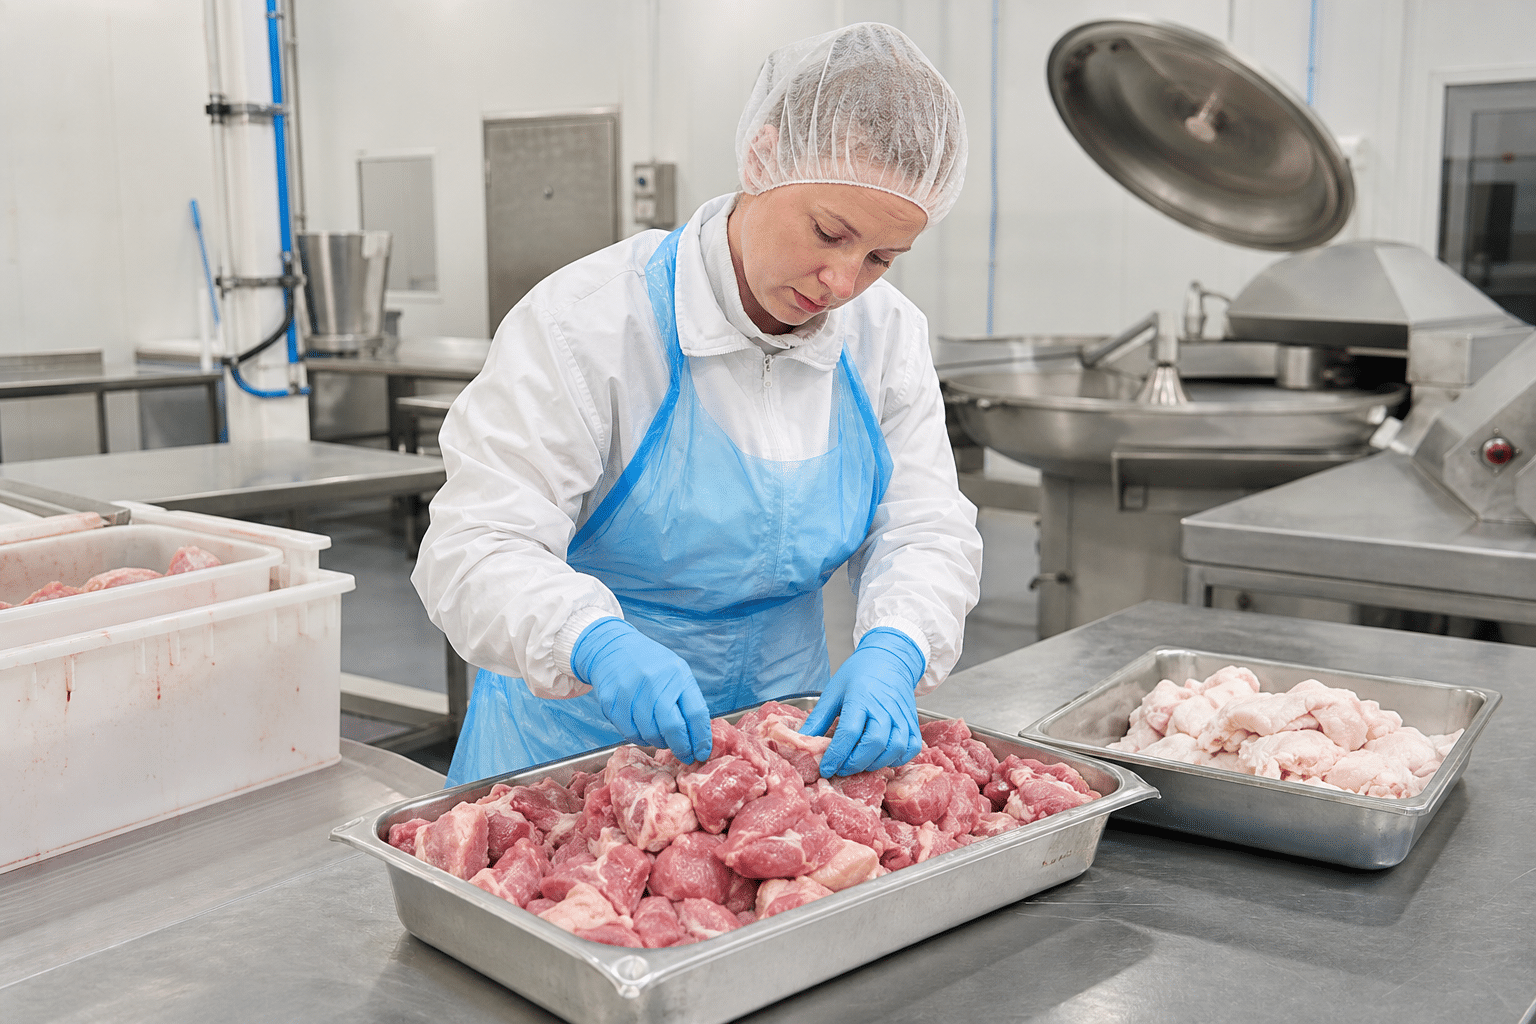
Good blade life starts at receiving and preparation, not at the cutter. Establish a simple pre-processing check so that operators do not use the bowl cutter as a substitute for trimming, deboning, thawing, or size reduction.

Remove hard material and packaging completely

Inspect incoming meat, fish, vegetables, and other raw materials for bone, shells, ties, labels, clips, and packaging fragments. Trim as required by the product specification. This step is particularly important when materials are transferred from boxed, vacuum-packed, or frozen storage formats.

Manage temperature and piece size

Use a product temperature and piece size that the cutter and recipe are designed to handle. An overly hard product can impact the blade rather than cut cleanly. Conversely, a soft or warm product may smear and encourage operators to lengthen the cycle unnecessarily. Cut large raw materials into manageable pieces before loading, and use only the approved method for tempering or thawing.

Use separate equipment where it improves preparation

Where meat must be portioned through bone or from frozen blocks, use equipment designed for that task before the product reaches the bowl cutter. The principles in this fresh versus frozen meat bone saw guide can help managers plan the correct upstream cutting method. A bowl cutter blade should not be expected to absorb the work of a saw or heavy-duty portioning process.

Also verify that spice blends, additives, and dry ingredients are free from damaged packaging and hard foreign matter. Use controlled scoops and closed containers where practical to reduce accidental contamination.

Use the Correct Cutting Process

Even a high-quality blade can lose its edge prematurely when the machine is run outside the approved process. Train operators to follow a documented sequence for each product rather than relying only on visual judgement.

  • Load batches within the machine’s stated working limits. Overloading can reduce circulation in the bowl and lead to longer cycles or uneven contact with the product.
  • Start with the speed and cutting stage specified for the recipe and equipment. Do not assume that maximum speed is the best setting for every ingredient.
  • Add ingredients in the planned order. For example, a recipe may require primary material to be cut first and dry or abrasive ingredients to be added later. The correct order depends on the formulation and the equipment instructions.
  • Stop the process once the required particle size, texture, or mix is achieved. Extra running time does not correct a dull edge and may increase product temperature or mechanical wear.
  • Do not reach into, scrape, or adjust the bowl while the machine is moving. Isolate power and follow the manufacturer’s safe shutdown procedure before any intervention.

Pay attention to changes in sound, vibration, cutting pattern, or processing time. These can indicate blade wear, incorrect loading, a loose component, or another condition requiring inspection. Routine safety and maintenance controls are also essential for other cutting equipment; review these commercial cutting equipment safety and maintenance protocols when developing site-wide practices.

Clean and Handle Blades Without Damaging the Edge

Cleaning protects hygiene and blade condition when it is done promptly and with the right tools. Residue left on the blade can dry and become difficult to remove, increasing the temptation to scrape aggressively. At the same time, cleaning must never place staff at risk from sharp edges.

First, stop the machine, isolate it from its power source, and wait until all moving parts have stopped. Follow the equipment manual for access, disassembly, and permitted cleaning procedures. Wear appropriate cut-resistant personal protective equipment where required by the site’s risk assessment.

  • Remove product residue with a soft brush, cloth, or approved non-metal tool.
  • Use cleaning chemicals at the concentration, temperature, and contact time recommended by both the chemical supplier and the equipment manufacturer.
  • Avoid wire brushes, grinding pads, and uncontrolled metal scrapers on sharpened edges.
  • Rinse and dry parts thoroughly where the cleaning procedure requires it. Do not leave blades soaking unless the equipment and chemical instructions permit this.
  • When blades are removed, place them in a dedicated protective holder or rack. Do not stack them loose in a sink, tray, or drawer.

Inspect the bowl and surrounding components during cleaning. A buildup of product, damaged seals, loose fittings, or wear that changes blade clearance should be addressed before the next production run. Cleaning also gives the operator the best opportunity to spot chips, corrosion marks, and damage near the blade mounting area.

Inspect Blades Before Wear Becomes a Production Problem

A short inspection at the start of each shift and during cleaning can prevent a small issue from becoming a damaged product batch or unplanned stoppage. The inspection should be visual and practical; operators should not touch or test sharp edges in an unsafe manner.

Look for the following signs:

  • Visible nicks, chips, bends, cracks, or corrosion.
  • An uneven edge or a bright, flattened line where the cutting edge should be sharp.
  • Loose fasteners, incorrect seating, or damage around the blade hub and mounting points.
  • Unusual clearance between blade and bowl, or evidence of contact such as scoring or metal marks.
  • A change in finished product appearance, including tearing, uneven particle size, or a need for longer processing.
  • Unexpected vibration, noise, or heat during operation.

Record the result of inspections in a simple maintenance log. Include the date, operator, product processed, observed condition, corrective action, and sharpening or replacement date. This creates useful evidence when deciding whether wear is normal, related to a particular ingredient, or connected to an operating practice.

If a blade is cracked, bent, severely chipped, loose, or suspected to have contacted metal, remove the machine from service in line with site procedure and have the issue assessed by an authorised technician or competent service provider. Do not attempt to straighten, weld, or improvise a repair to a food-processing blade.

Sharpen or Replace Blades at the Right Time

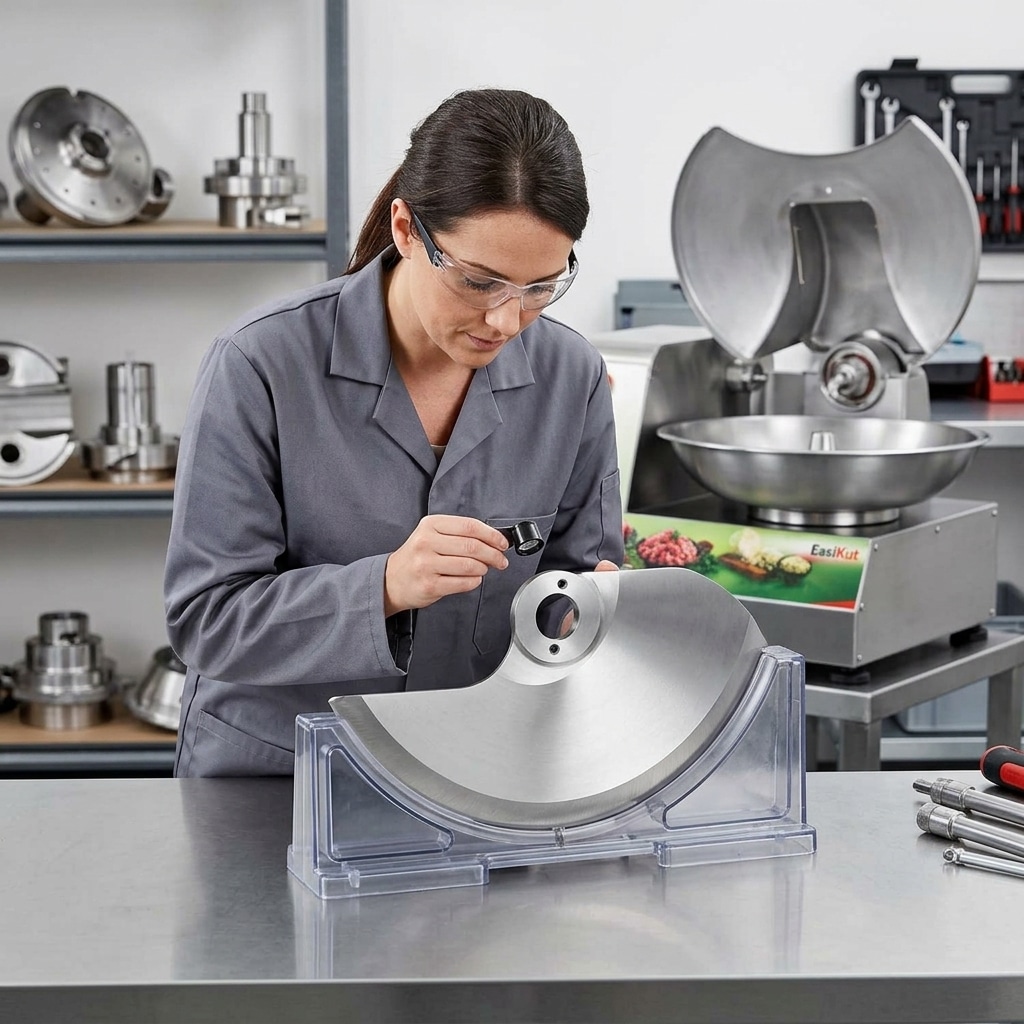
Bowl cutter blade secured for professional inspection

Sharpening restores a blade only when the blade remains structurally sound and within the manufacturer’s permitted service limits. It is not a solution for every defect. A professional sharpening provider should preserve the correct edge geometry, balance, finish, and mounting condition required for the specific blade.

Arrange an assessment when operators consistently observe slower cutting, reduced product uniformity, tearing instead of clean cutting, or a need to extend a previously proven process. Do not wait until the blade is heavily damaged. Continued operation with a dull blade can make the process less consistent and may cause operators to use unsuitable workarounds.

Before sending blades for sharpening, identify them clearly and keep sets together where applicable. Confirm with the machine supplier or blade provider:

  • the correct blade part number and intended application;
  • the permitted sharpening method and minimum service condition;
  • whether blades should be sharpened as a matched set;
  • the correct reinstallation and torque procedure; and
  • the inspection steps required before returning the machine to production.

Replace a blade when it has damage that cannot be safely corrected, has reached its permitted sharpening limit, no longer mounts correctly, or cannot deliver the required process result after approved service. Keep a documented spare-blade plan so that a necessary replacement does not turn into a rushed purchasing decision.

A Practical Blade Maintenance Routine

A clear routine is more reliable than waiting for an operator to report a problem. Adapt the following framework to the machine manual, product types, sanitation programme, and local food-safety requirements.

Before each shift

  • Confirm the machine is clean, correctly assembled, and free of loose parts.
  • Visually inspect blades, mountings, bowl condition, guards, and covers.
  • Verify that raw materials have been prepared according to the product specification.
  • Check that the operator understands the recipe sequence and safe stopping procedure.

During production

  • Monitor product texture, process time, sound, and vibration.
  • Do not process questionable material containing bone, packaging debris, or unknown hard objects.
  • Stop and investigate abnormal conditions immediately.

After each production period

  • Shut down and isolate the machine before cleaning.
  • Remove residue using approved tools and complete the sanitation procedure.
  • Inspect the blades again while the equipment is accessible.
  • Record defects and actions in the maintenance log.

At planned service intervals

  • Review sharpening history, replacement history, and recurring defect reports.
  • Check blade mounting hardware, bowl condition, clearances, and related components as specified by the manufacturer.
  • Arrange professional service when inspection results, production results, or the manual indicate it is due.

Keep the manufacturer’s manual available at the point of use. If instructions are missing or unclear, request the correct documentation before changing blade type, sharpening method, or assembly procedure.

Common Mistakes That Shorten Blade Life

Many blade-life problems are avoidable. The following practices should be corrected through training, supervision, and written procedures.

  • Using the cutter to process unsuitable hard material: Remove bone and foreign objects upstream instead of assuming the blade can tolerate occasional impacts.
  • Adding ingredients without a defined sequence: Abrasive dry ingredients or hard inclusions may need a particular timing. Follow the approved recipe.
  • Running longer when texture is poor: Check the blade, product preparation, and batch loading rather than automatically adding time.
  • Cleaning with whatever tool is available: A metal scraper or wire brush can harm an otherwise serviceable edge.
  • Storing removed blades unsecured: Loose storage creates risk to personnel and can cause edge-to-edge impact damage.
  • Ignoring minor changes: A small chip, unusual sound, or scoring mark is easier to address before it becomes a larger mechanical problem.
  • Using an unverified sharpening method: Improper grinding can alter edge geometry, create excess heat, or affect blade balance.

Similar discipline applies to other commercial cutting tools. For example, saw blades must match the intended machine and product type; this commercial meat band saw blade selection guide explains why blade application should be confirmed before operation. Do not transfer a sharpening practice or operating assumption from one machine type to another without checking the relevant manual.

Protect Blade Life and Product Consistency

Effective bowl cutter blade maintenance is a controlled operating system: prepare ingredients properly, keep hard contaminants out of the bowl, run approved batches and sequences, clean without abrasion, inspect routinely, and use qualified sharpening or replacement service when performance declines.

There is no universal sharpening interval because wear depends on the blade design, ingredients, product condition, batch pattern, operating method, cleaning practice, and equipment model. Use inspection findings and documented production results instead of a guessed schedule. For model-specific blade information, service limits, and assembly instructions, follow the documentation supplied with the machine.

A well-managed blade programme helps the operation maintain a predictable process while giving supervisors clearer information for training, maintenance planning, and spare-parts control.